Welcome to visit our factory
Email : info@huasuicrane.com

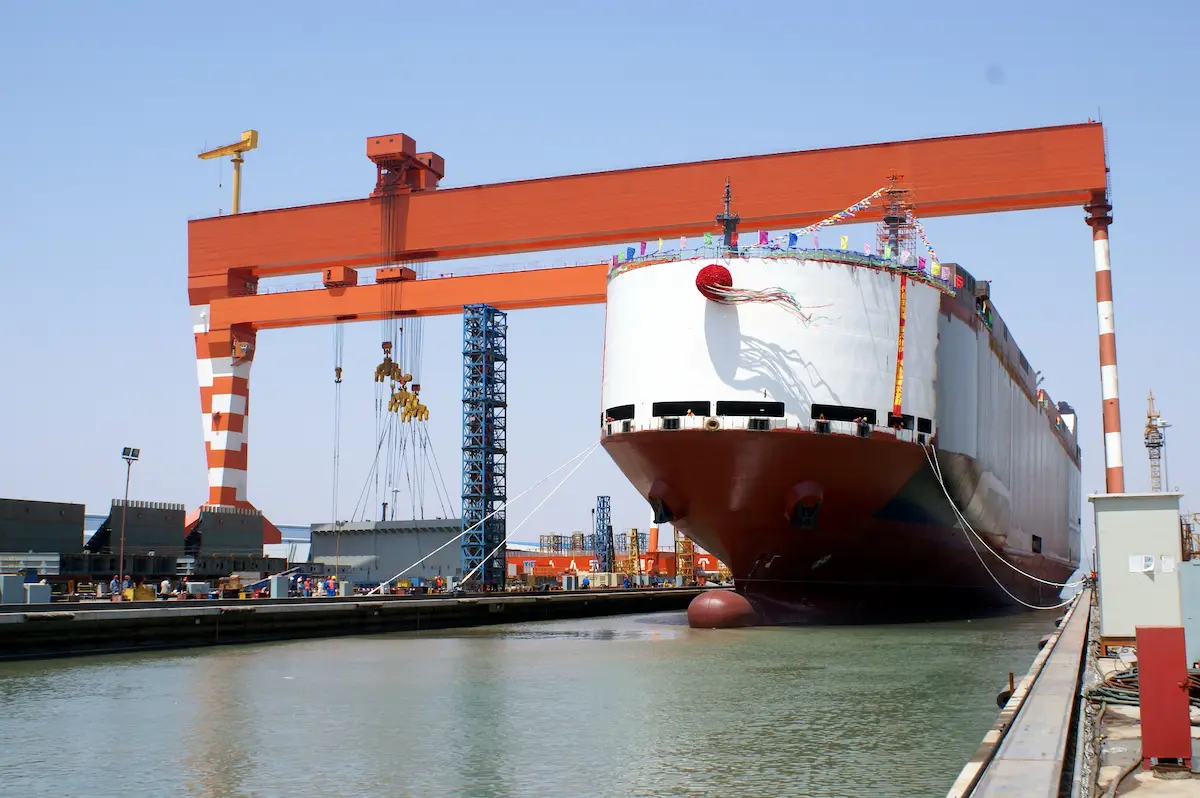
In modern shipbuilding, ship sizes and modular layouts continue to expand. A shipyard gantry crane is no longer a simple handling tool. It serves as core equipment that directly determines shipyard capacity and precision. From steel cutting to block assembly, every load shift requires its steady support. Modern shipbuilding breaks down large vessels into hundreds of mega blocks. These blocks are prefabricated in workshops and transported to dry docks for assembly. However, rising ship tonnages push block dimensions and weights to record levels. This presents unprecedented challenges for on-site lifting operations. Center-of-gravity shifts, unequal slinging loads, and wind interference all pose strict challenges. Millimeter-level alignment precision severely tests lifting equipment performance and command coordination. Under these demanding conditions, large gantry cranes demonstrate indispensable value. They handle heavy block lifting, transfer, and mid-air turning duties. They also utilize multi-trolley coordination and micro-motion controls to ensure positioning safety. Following real-world workflows, this article breaks down lifting and assembly procedures. It reveals the core secrets behind modern shipyard heavy lifting operations.
Planning large hull block lifting or shipyard assembly projects?
HSCRANE provides customized gantry crane solutions based on block weights, working spans, lifting heights, and shipyard site conditions.
[Click here to consult shipyard gantry crane solutions]
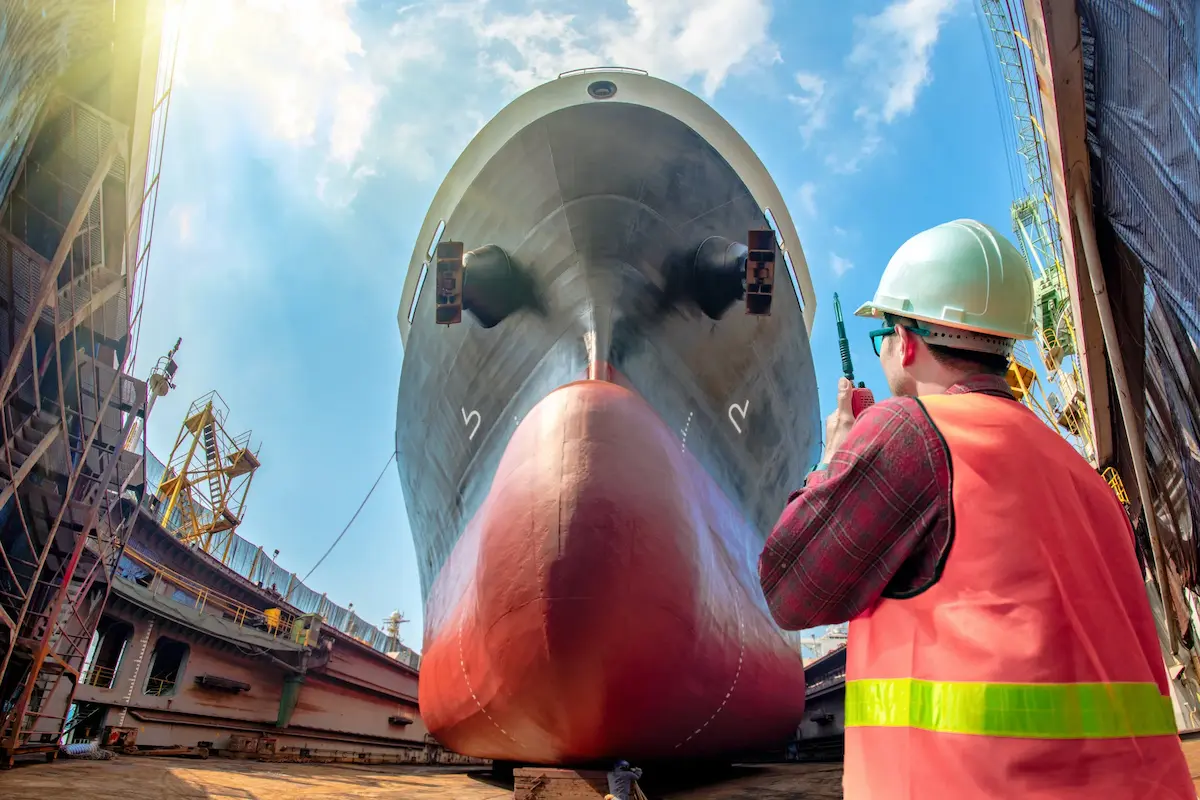
In daily shipyard operations, block lifting and assembly is never a simple hook-and-go task. It is a high-risk operation requiring strict logic and multi-party coordination. Every step from shop assembly jigs to dry docks must proceed systematically.
Before the shipyard gantry crane lifts, site personnel must thoroughly check all operational factors. Any overlooked parameter could trigger irreversible consequences during mid-air operations. For operator convenience, key pre-lifting checks are summarized in the checklist below:
|
Inspection Dimension |
Core Verification Items |
Technical / Safety Standard Requirements |
Responsible Party Confirmation |
|
Hull Block Parameters |
Verify actual weight, dimensions, theoretical center of gravity, and reserved lifting points |
Weight must not exceed design estimates; lifting points must be reinforced; changing lifting positions is prohibited |
Hull Process Engineer / QC Inspector |
|
Crane Equipment Status |
Rated lifting capacity, main and auxiliary hook heights, span, and travel distance |
Actual load must not exceed rated capacity; all limiters and safety protection devices must function reliably |
Crane Operator / Equipment Manager |
|
Rigging and Connectors |
Dedicated spreader beams, steel wire ropes, shackles, and shackle pin shafts |
Rigging requires qualification certificates and inspection reports; wire ropes must be intact; pins must lock properly |
Rigging Team Leader / Safety Officer |
|
Plan and Personnel Coordination |
Lifting sequence, transfer route, site labor division, and wireless communication channels |
The plan requires approval from technical and safety departments; complete technical disclosures to all workers |
Site Chief Commander / Safety Officer |
|
On-site Working Environment |
Track laying, foundation capacity, path obstacles, and wind speed |
Tracks must be clear; foundation must show no settling; wind speed must stay below safe threshold limits |
Weather Observer / Site Commander |
After plan approval, site hooking begins. Hooking staff must connect wire ropes, shackles, and lifting lugs strictly per approved drawings. One key point must be emphasized: never lift directly based on estimated weights or experience alone. Large hull block structures are often asymmetric. Welding slag, water, or temporary stiffeners inside blocks can alter actual weights and gravity centers. After connecting all rigging, a trial lifting procedure must be executed:
Only after confirming stable block attitude and normal equipment status can the chief commander give formal lifting instructions.
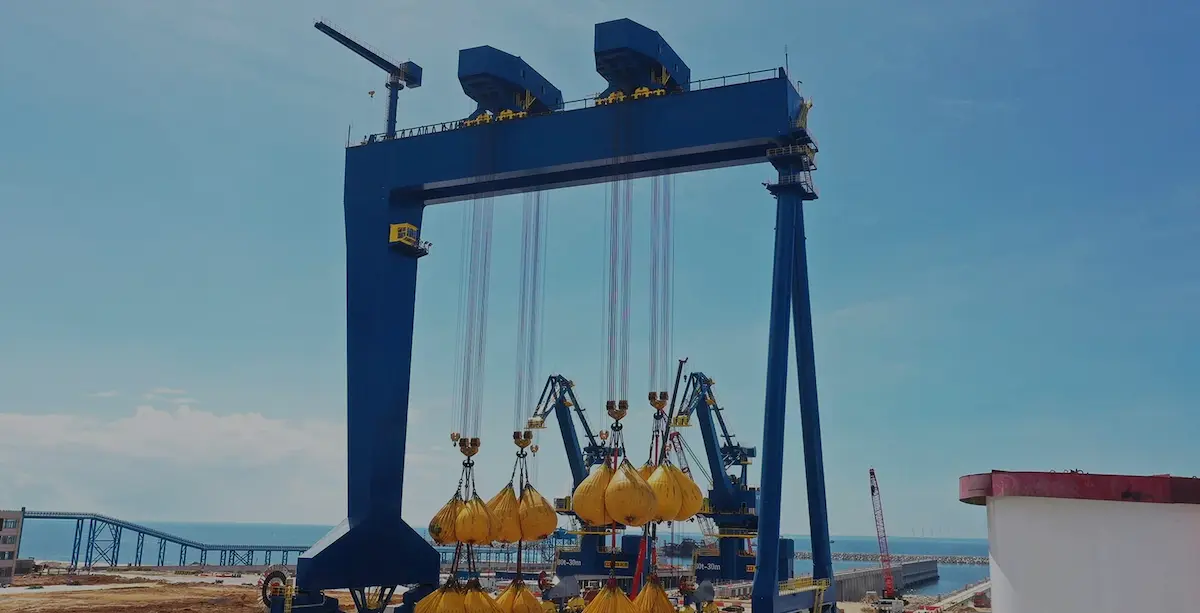
After trial lifting, the crane smoothly lifts the block above obstacle heights. It then begins horizontal transport toward the block assembly area. Moving heavy components in the air requires avoiding sudden stops and swinging. Smooth operation relies on device performance and driver skills during this path:
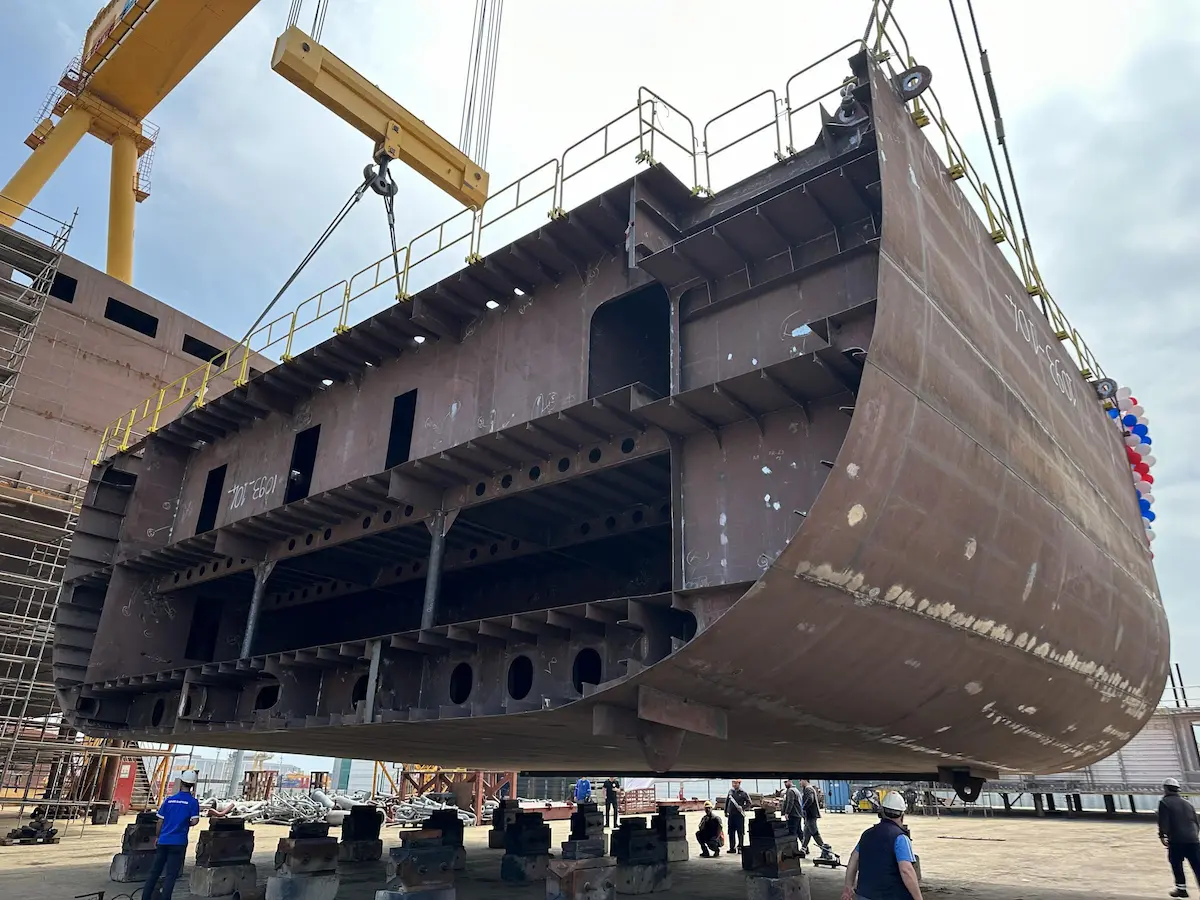
In shipbuilding, many blocks are built upside down or sideways. Before reaching assembly sites, they require 90° or 180° mid-air turning.
Special Note: Mid-air turning is a high-risk operation, and not every shipyard gantry crane supports it. Only cranes equipped with dual trolleys and dedicated turning systems can perform mid-air turns after scheme validation.
Specific steps for turning operations:
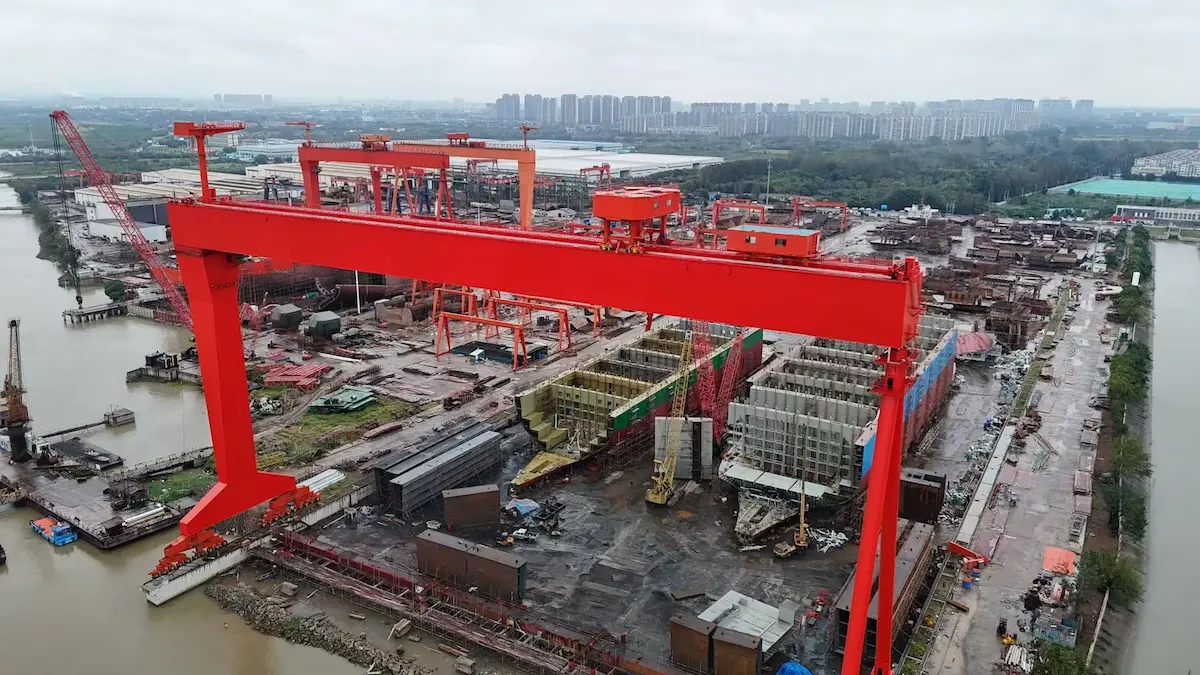
After reaching the dry dock, blocks enter a millimeter-precision docking phase. Docking requires close cooperation between crane drivers, survey personnel, and assembly workers:
[Lower block above location]
│
▼
[Check baseline and markers] ──(Surveyors track using total stations)
│
▼
[Enable micro-motion mode for lowering] ──(Millimeter-level fine adjustments)
│
▼
[Re-check gap and alignment offset]
│
▼
[Install temporary stoppers and dog plates]
│
▼
[Gradually transfer loads to hull structures/supports]
During this phase, micro-motion controls (typically operating at 0.1–0.5 m/min) play a decisive role. Drivers make minute adjustments using real-time feedback from surveyors to align plate edges, stiffeners, and webs.
After alignment, assembly workers spot-weld temporary positioning dogs and tensioners to secure the block and prevent movement.
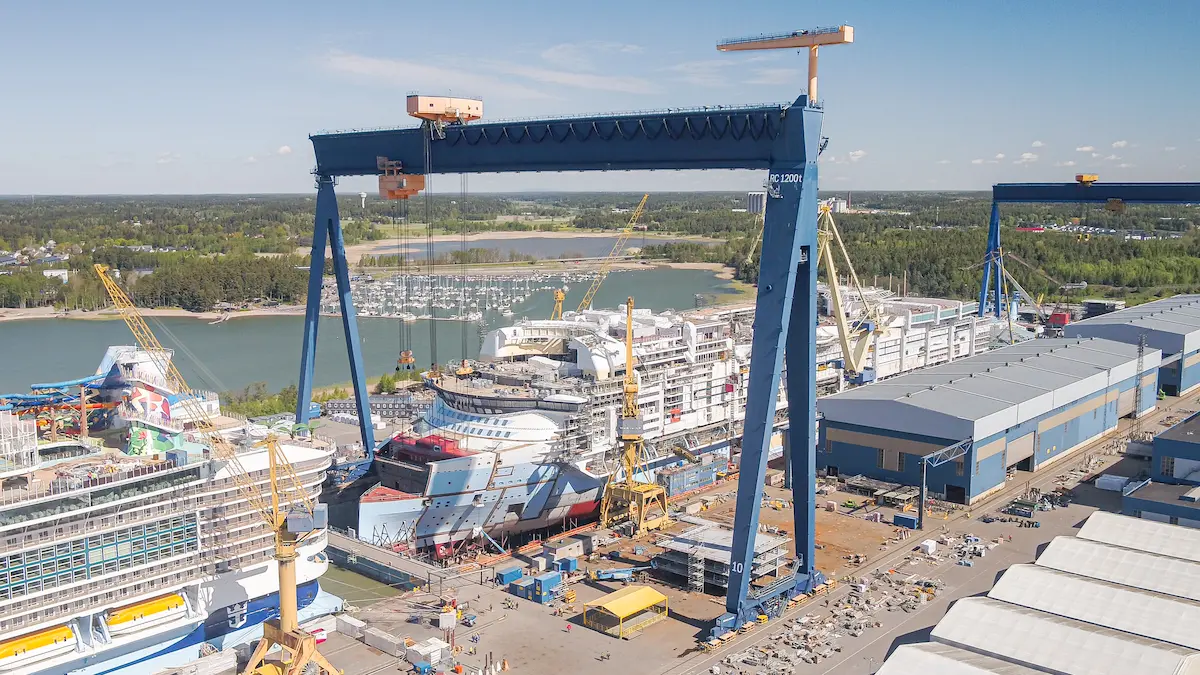
The crane can unload only after temporary welding finishes and support structures safely bear the block weight.
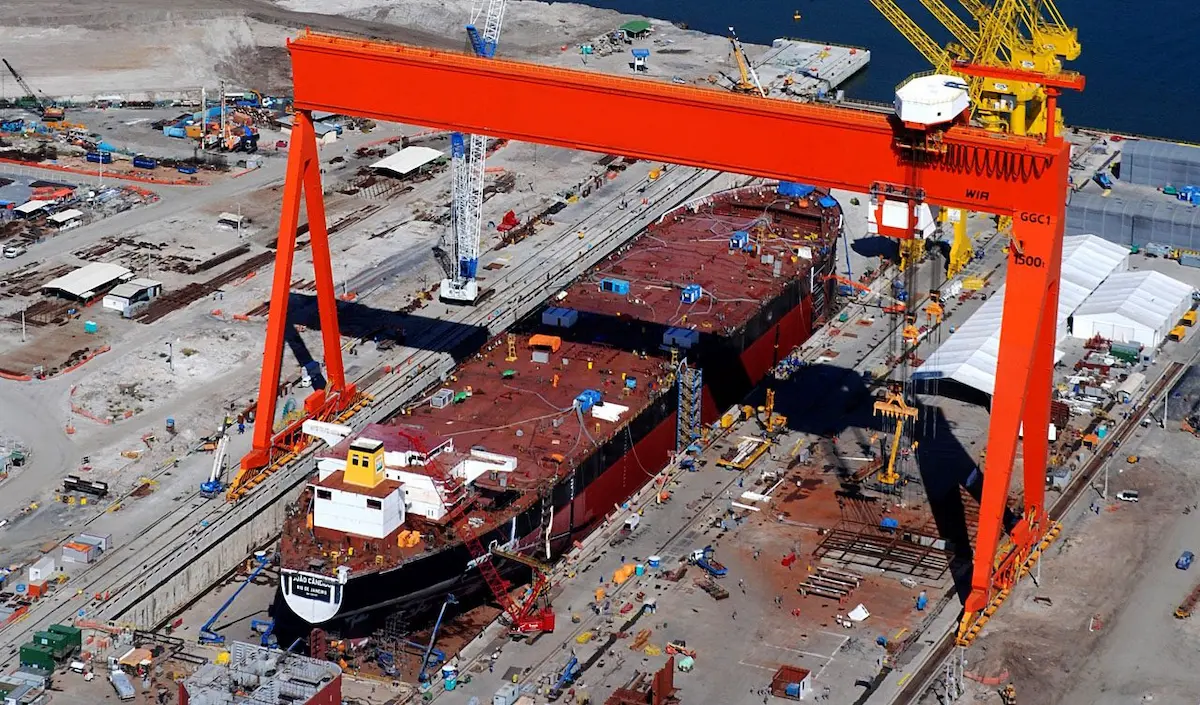
Selecting a shipyard gantry crane impacts initial budgets and long-term assembly efficiency. Key dimensions include:
|
Selection Dimension |
Core Technical Basis |
Engineering Guidelines |
|
Lifting Capacity |
Block and rigging weight with margins |
Calculate using peak block weights for target vessels over 5–10 years. Keep routine loads at 75%–85% capacity. |
|
Span & Height |
Dock width and stacked block height |
Span: Cover dock width and side yards. Height: Maintain 2m safety clearance above assembled structures. |
|
Trolley Setup |
Block turning and load balance |
Use dual trolleys for air-turning; choose single trolleys for translation to reduce cost. |
|
Control & Protection |
Micro-speed and corrosion class |
Require 0.1–0.5 m/min micro-speeds, ISO 12944 C5-M/CX coatings, and positive-pressure electrical rooms. |
Why Customized Design Is Critical for Shipyard Gantry Cranes
Shipyards feature non-standard layouts with unique dock dimensions, foundation limits, wind conditions, and prefabrication workflows. Standard off-the-shelf crane models create severe operational risks. Incorrect wheel-load calculations lead to rail collapse or foundation settlement. Mismatched lifting heights or trolley configurations leave cranes partially idle when unable to execute required mid-air block turning. Deep customization provides the only path to ensure seamless operational integration.
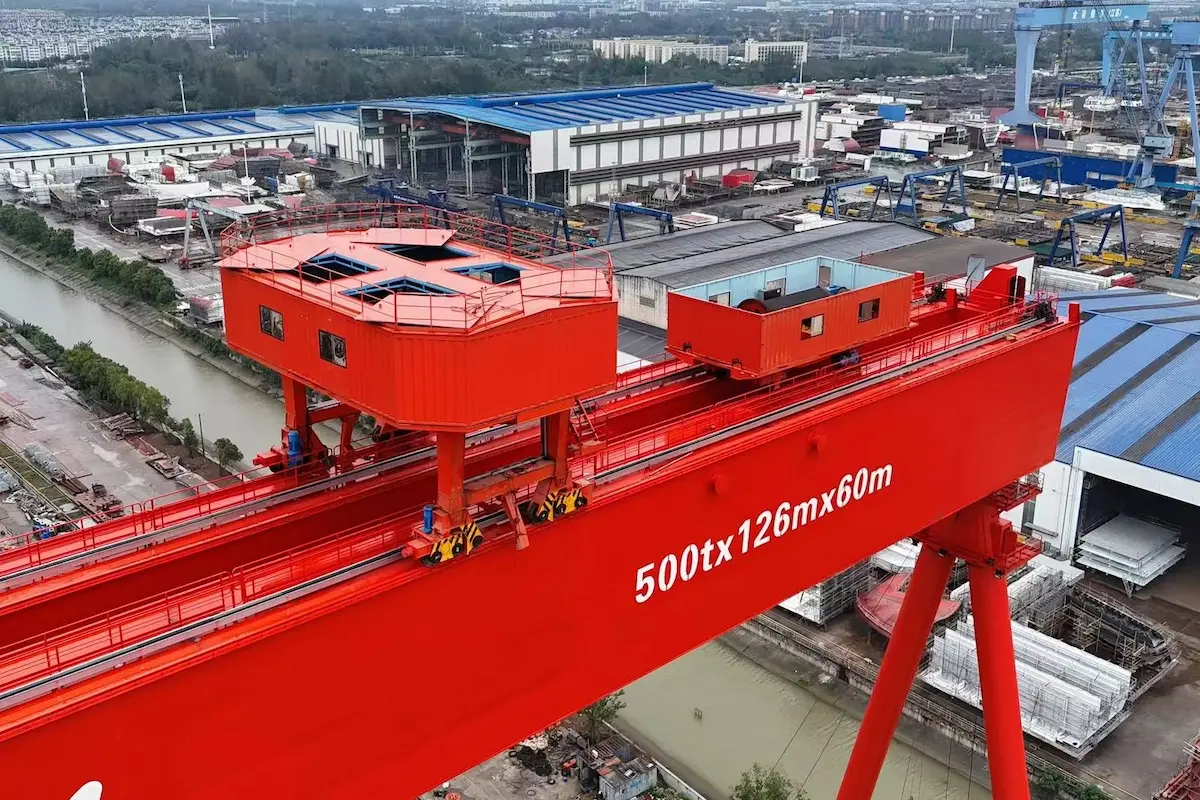
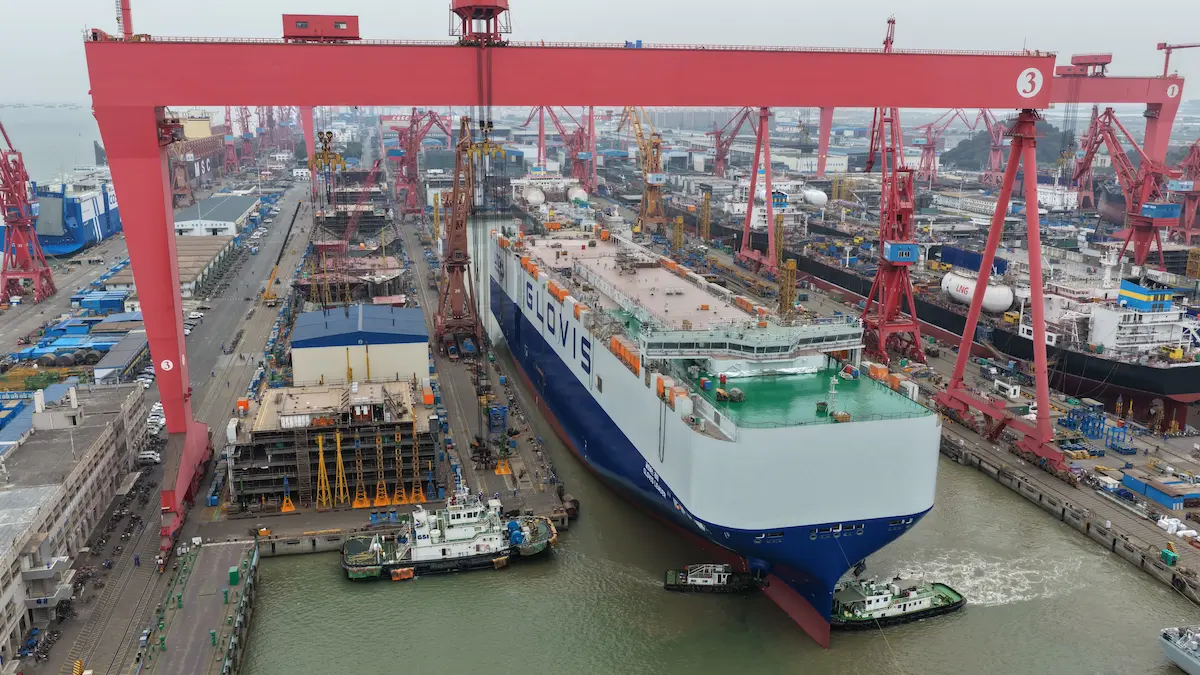
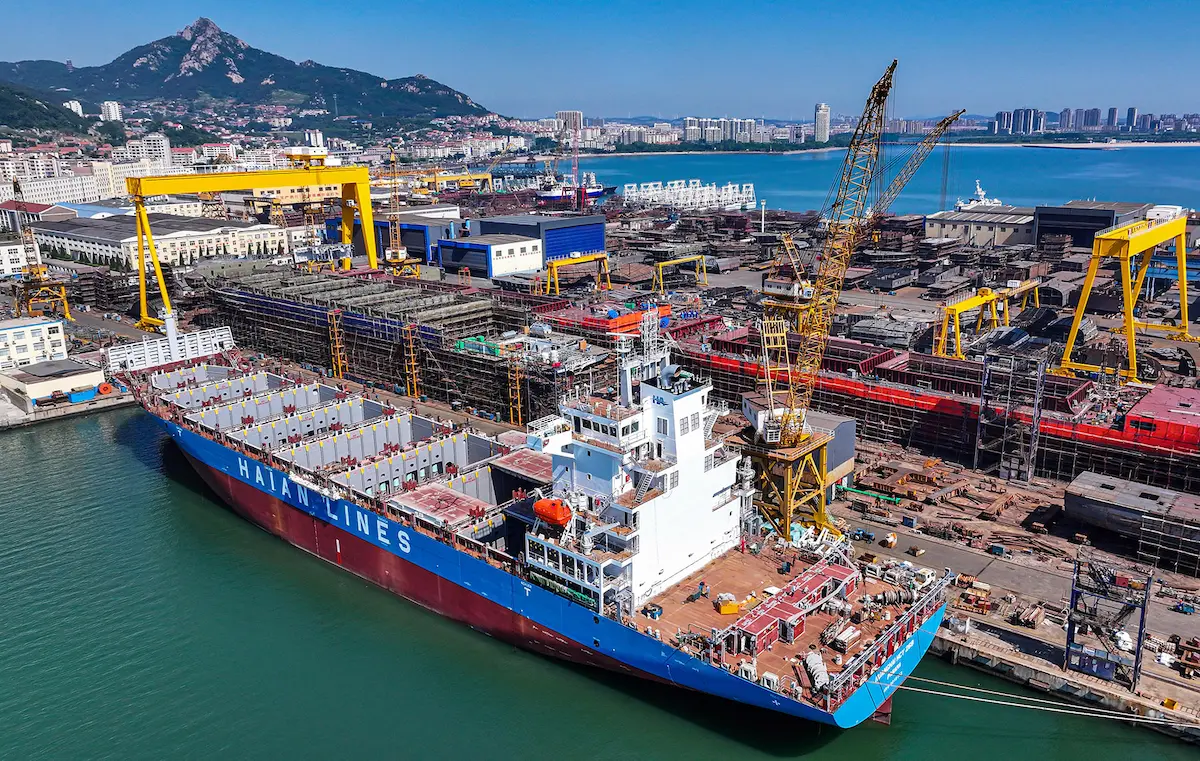
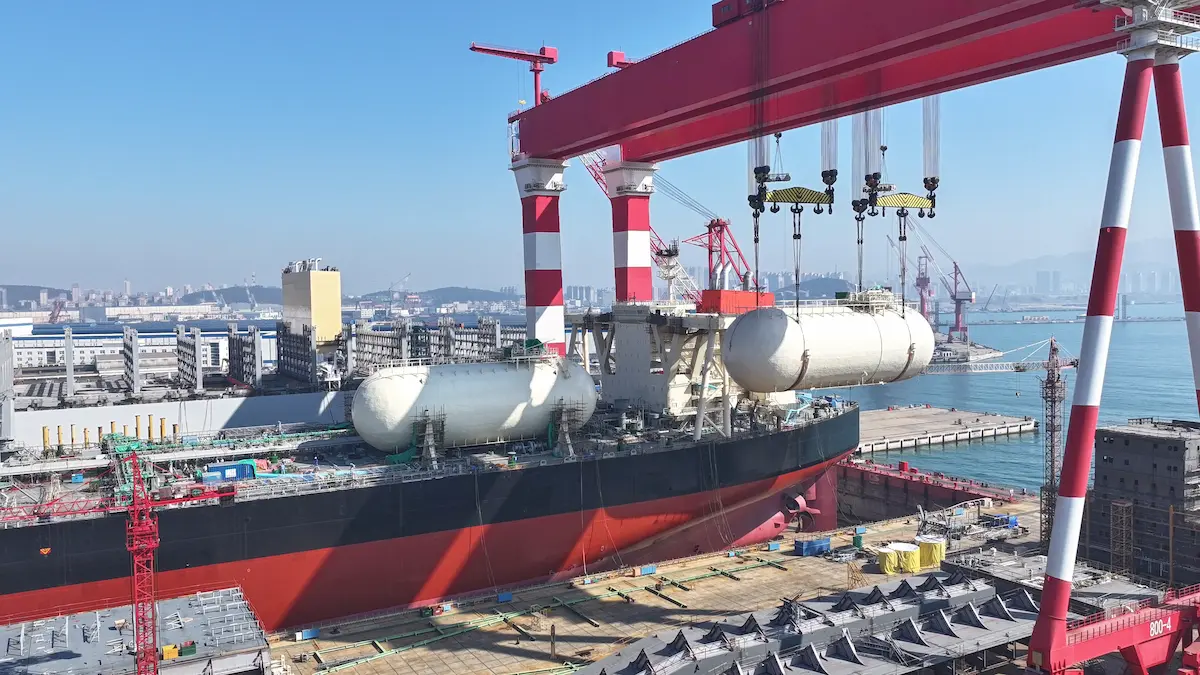
Lifting and assembly of large hull blocks represent an air relay testing shipyard technology and equipment capabilities. Every step—from rigorous parameter checks and cautious trial lifting to smooth air transport and high-precision micro-motion docking—relies on performance support from a shipyard gantry crane. It is not only heavy equipment boosting shipyard productivity, but also the baseline securing site operations.
For shipyards seeking capacity upgrades or constructing new docks, selecting the right crane produces double the results with half the effort. Choosing a shipyard gantry crane with high-precision control, strong corrosion resistance, and customized design capabilities drastically shortens shipbuilding cycles while laying a solid foundation for decades of safe, efficient production.
Facing challenges during selection or technical retrofits for your shipyard gantry crane?
HSCRANE possesses rich global shipyard project experience. We deliver customized, efficient, and reliable heavy lifting solutions tailored to your dry dock dimensions, block tonnages, and process requirements. Contact our engineering team today.
[Click here to submit project details or contact the HSCRANE technical team]
Further Reading:
Air scheduling of large hull blocks is only a snapshot of gantry crane performance. To learn how gantry cranes tackle complex outdoor climates, ultra-wide spans, and heavy component handling across heavy manufacturing sectors, read further:
[Click to read] How Gantry Cranes Handle Heavy Outdoor Loads in Equipment Manufacturing
Q1: What are core differences between a shipyard gantry crane and a standard double-girder gantry crane?
A1: A shipyard gantry crane features larger spans and lifting heights, utilizing dual trolleys or multi-hook structures. It includes mid-air block turning logic and millimeter-level micro-motion systems. Built for coastal shipyards, its anti-corrosion protection (ISO 12944 C5-M) and wind anchoring far exceed standard industrial cranes.
Q2: What trolley setups are required for mid-air block turning operations?
A2: Mid-air turning relies on multi-hook coordination, typically configured with upper dual hooks and lower single/auxiliary hooks. Upper and lower trolleys shift on offset tracks while independent differential hoisting controls tilt blocks smoothly past gravity centers to complete 180° turns. Single-trolley cranes must never perform heavy mid-air turning.
Q3: How to extend crane service life in coastal environments with high salt mist and frequent gusts?
A3: Apply high-zinc epoxy primers with fluorocarbon topcoats reaching C5-M/CX corrosion ratings. Enclose electrical cabinets inside positive-pressure rooms with temperature and humidity controls. Equip travel tracks and open machinery with windproof rail clamps, anchoring devices, and regular grease maintenance.
Q4: Can a larger capacity gantry crane be installed if existing rail foundation load capacity is limited?
A4: Yes, through customized structural engineering. Manufacturers optimize main girders and increase wheel counts (e.g., from 16 to 32 wheels) to distribute wheel loads evenly. This boosts lifting capacity while keeping wheel pressures strictly within existing track load limits.
This document is for reference only. Specific operations must strictly comply with local laws and regulations and equipment manuals.